








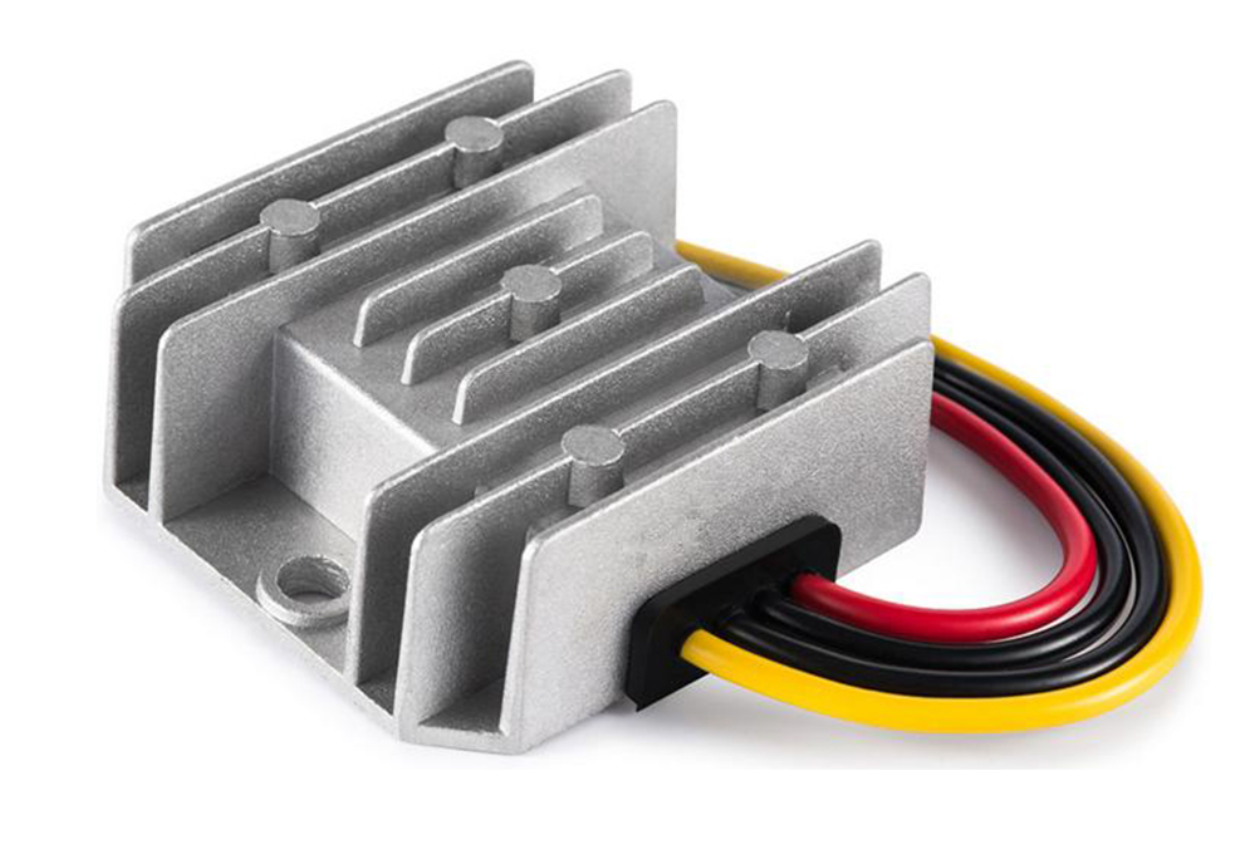
Release a DC-DC converter module to production only after its exact package is qualified for the proposed assembly process. Electrical input and output ratings do not establish reflow permission, cleaning compatibility or reuse after removal. Match the manufacturer’s applicable package instructions to the board process, materials and traceable rework history.
On this page
- Identify the assembly type before discussing temperature
- Build a process window from the exact documents
- Treat washing as a package-specific decision
- Assess adhesive, coating and potting separately
- Keep rework history with the module
- Requalify the affected boundary after changes
- Request the right manufacturing documents
This is a manufacturing-release checklist for an OEM evaluating a converter. It does not establish that a WEHO wired converter is a solderable board module, or prescribe one soldering temperature for every package sold as a “DC-DC module.”
Identify the assembly type before discussing temperature
Record the complete part number, suffix, package drawing, terminal finish and manufacturer document identity. A through-hole pin module, a surface-mount package and an enclosed unit with leads can require entirely different attachment methods. Similar voltage ratings or body dimensions do not make their manufacturing instructions interchangeable.
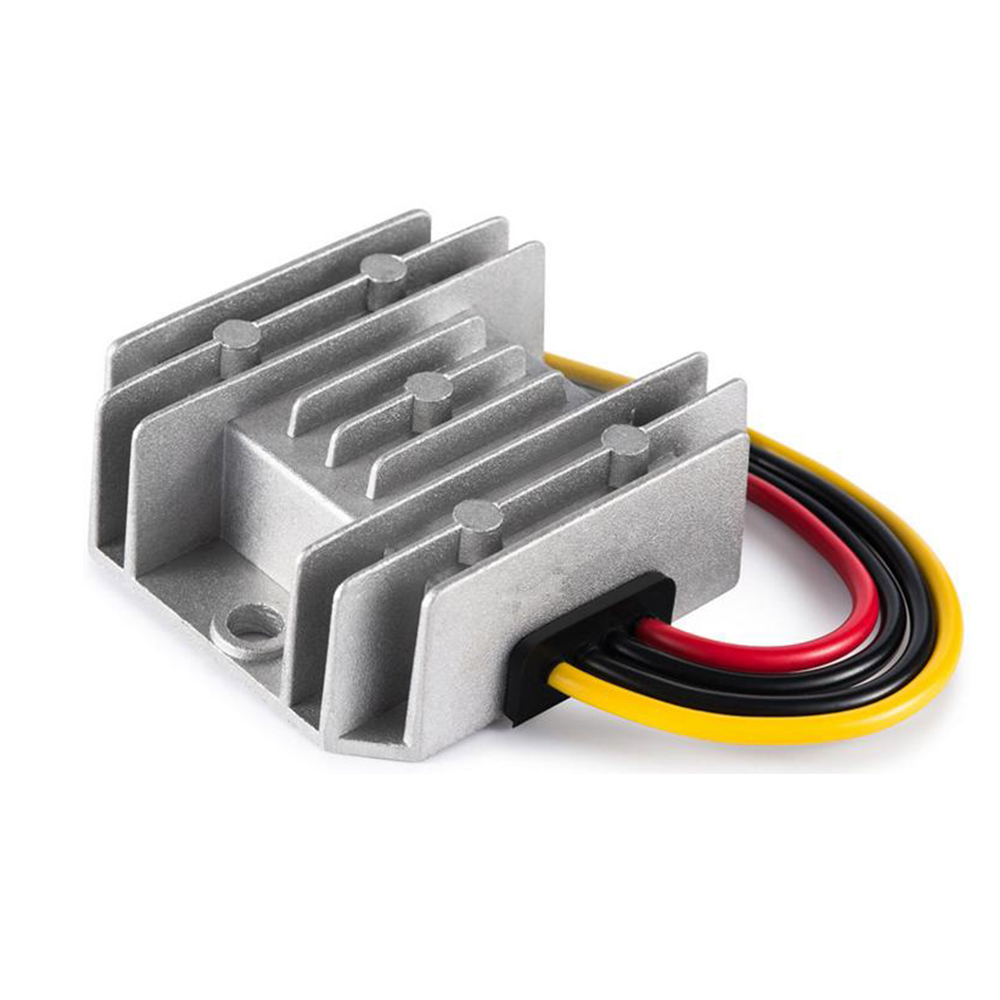
For a concrete scope check, the WEHO WH-C241205 product information και model sheet describe a fully sealed converter with external input/output leads. That is a different assembly identity from the solder-down packages discussed in the manufacturing examples below. The reviewed WEHO documents do not supply a PCB reflow profile or a cleaning/rework process for this product. Request instructions for the actual termination and material exposure instead of applying a different module’s process to the pictured unit.

Vicor’s PI31xx AN:302 is explicitly a family-specific reflow guide. It discusses storage, board considerations, reflow, inspection and rework for the covered products. Its existence shows the kind of controlled manufacturing information to obtain; its profile and process limits are not specifications for another converter.
Build a process window from the exact documents
Ask which attachment methods are permitted and which measurements define their limits. An oven’s programmed temperature is not automatically the module-case or solder-joint temperature. The board’s thermal mass, nearby components and fixture can change the profile seen by the module.
Prepare a representative assembly and instrument the locations required by its instructions. Compare the recorded process against the applicable limits for peak, time, ramp behavior and number of exposures. Keep the measured profile, board revision, process recipe and material identities together so a production change can be assessed against the original release.
| Release field | Record for the exact module | Evidence to retain |
|---|---|---|
| Package and finish | Part/suffix, footprint, terminal finish and permitted attachment method | Applicable drawing and assembly instruction |
| Thermal process | Required measurement locations and permitted temperature/time history | Recorded profile on the representative assembly |
| Moisture handling | Applicable storage, exposure tracking and conditioning requirements | Lot handling and approved conditioning record |
| Cleaning and finishing | Flux, wash chemistry, drying, adhesive or coating process | Compatibility evidence and qualified process configuration |
| Inspection and rework | Joint/package acceptance, removal/replacement permission and exposure history | Inspection results and serial/lot traceability |
Do not replace missing process information with a temperature taken from a neighboring component’s datasheet. Escalate the affected operation until the supplier identifies the applicable conditions. Other design work can continue, but the unsupported manufacturing step should not silently become the default factory recipe.
Treat washing as a package-specific decision
Different manufacturer instructions can lead to different answers. The Vicor VI-200/VI-J00 guide, section 22 restricts liquid exposure of the covered modules and discusses a socket-based sequence where a board requires washing. That is a restriction for its scope, not a universal statement that all power modules are unwashable.
By contrast, Vicor AN:009 for SMT J-lead VI Chip packages discusses compatible water-wash procedures, residue-related reliability concerns and solvent compatibility review. These different package instructions are exactly why an assembler should not rely on a generic “sealed” or “no-clean” description.
Identify chemistry, concentration, bath temperature, duration, pressure or agitation, rinse and drying as applicable to the proposed process. Ask the supplier about the exact combination rather than requesting a broad “washable” label. Include any later heating operation in the assessment because processing can change the package’s moisture condition.
Assess adhesive, coating and potting separately
A wash-compatible package is not automatically compatible with an adhesive, conformal coating or potting compound. Material contact, curing conditions, thermal effects and any interaction with openings or movable components need a defined review. A supplier’s generic operating-temperature range does not approve the curing process.
Murata’s power-products operating requirements include material/environment cautions and identify a particular silicone-related concern. That supports asking for material compatibility; it does not establish a universal recipe or approve a chemical for WEHO products. Provide the actual material datasheet and process conditions to the responsible manufacturer.
Keep rework history with the module
Distinguish touch-up of a joint, a neighboring-component repair, module removal and module reuse. Each can impose a different thermal or mechanical history. Permission for initial attachment does not establish permission for all subsequent operations. Follow the exact package’s rework instructions and document any restriction on reusing removed parts.
For a hypothetical traveler, module A undergoes its original attachment and later experiences two additional board heating events during repairs. Record three events, their relevant measured conditions and the package’s applicable allowance. The count alone does not prove that three are permitted, that all events are equivalent, or that the part remains acceptable.
If an event was not recorded, do not reset its history by assigning a new board serial number. Isolate the affected assembly for a documented disposition. A functional output check can be useful, but it is not by itself evidence that an unqualified thermal or mechanical exposure caused no latent damage.
Requalify the affected boundary after changes
Review changes to module suffix, terminal finish, board copper, solder material, fixture, oven, wash chemistry or finishing compound against the released process. Retain the evidence that supports the change and repeat the affected verification. A supplier substitution should not inherit the previous module’s assembly approval from matching electrical ratings.
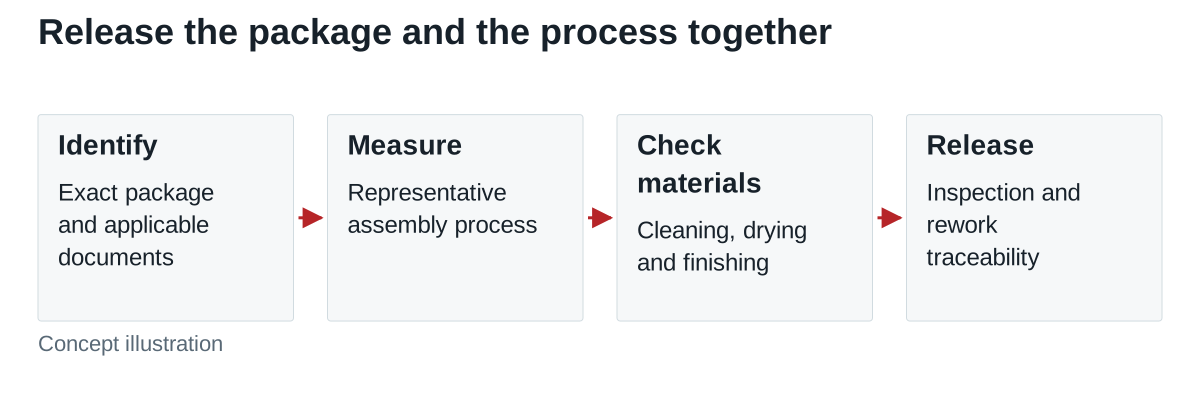
Use inspection criteria and electrical tests appropriate to the part and application, with the manufacturer’s specified methods. Record acceptance and rejected conditions consistently. A cosmetic photograph alone is not a complete solder-joint or package-integrity assessment, and an illustrative process flow is not a temperature profile.
Request the right manufacturing documents
Send WEHO the proposed converter identity, attachment concept, board/process information and planned washing, coating or rework operations. First confirm whether that product format supports the intended assembly method, then request the applicable package and processing documents. Keep unresolved steps visible in the manufacturing release record.